Preheating flame, an oxygen cutting jet that keeps a constant burning rate, a suitable torch assembly, and a gas supply system that is customized to the application are required for carbon HHO steel cutting machine. The industrial oxyhydrogen cutting solution developed by PTXSON is based on an industrial onsite hydrogen-oxygen gas supply back-up preheating flame and oxygen supply for cutting jet.
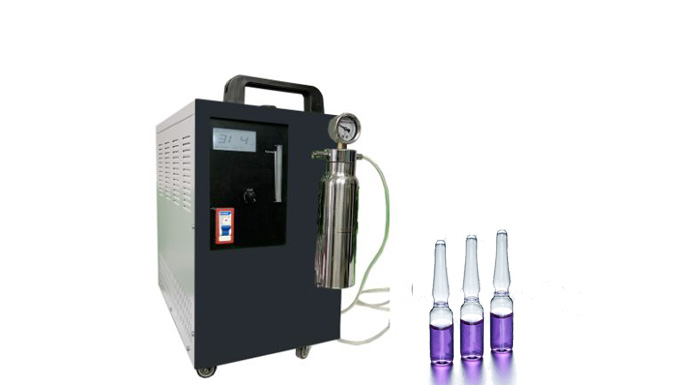
Here an oxyhydrogen generator for cutting is used and hydrogen oxide gas is generated out of water and electricity. A suitable cutting torch is used for the generated gas and the pre-heating flame is the pre-heating torch. In order to accomplish the task of oxidizing and removing the heated carbon steel material, a high-pressure cutting oxygen cylinder or supply is needed.
This configuration provides an alternative fuel-supply configuration to the industrial buyer for the cutting of carbon steel using oxyhydrogen cutting, in addition to the accepted principle used in oxygen-jet cutting.
Here an oxyhydrogen generator for cutting is used and hydrogen oxide gas is generated out of water and electricity. A suitable cutting torch is used for the generated gas and the pre-heating flame is the pre-heating torch. In order to accomplish the task of oxidizing and removing the heated carbon steel material, a high-pressure cutting oxygen cylinder or supply is needed.
This configuration provides an alternative fuel-supply configuration to the industrial buyer for the cutting of carbon steel using oxyhydrogen cutting, in addition to the accepted principle used in oxygen-jet cutting.
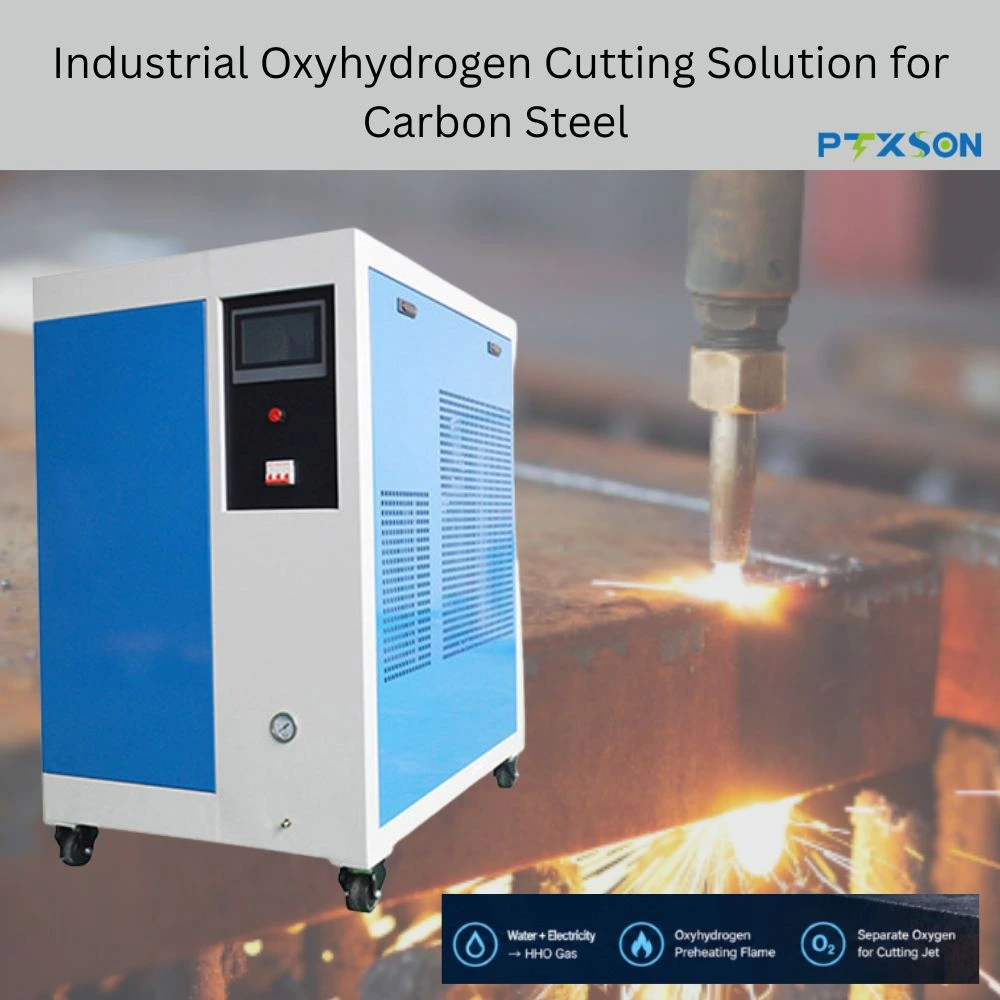
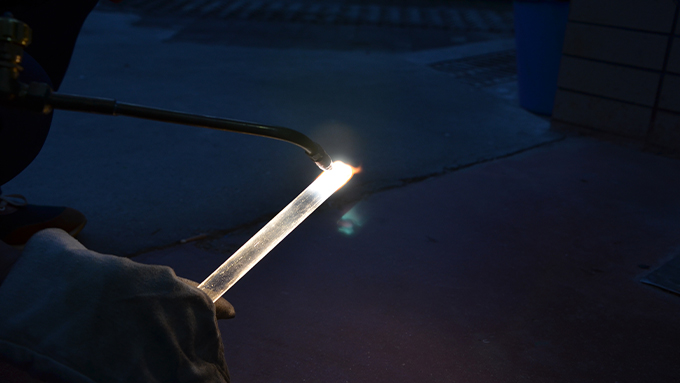
Oxyhydrogen flame cutting for structural steel is a thermal cutting process which uses the oxyhydrogen flame to preheat carbon steel prior to cutting using a separate high-pressure oxygen jet.
This process is carried out through a pre-heating and oxidation process with control. Firstly, the oxygen and hydrogen mixture oxyhydrogen flame brings the selected region of carbon steel to the desired temperature. After reaching a sufficient temperature, a focused jet of cutting oxygen is injected into the steel helping to cut the metal. The oxygen combines with the hot steel, creates oxides of iron and the hot pressure of the oxygen stream blowst the resulting oxides out of the kerf.
The cutting action is not to be interpreted as being the cutting function of the oxyhydrogen gas itself, so HHO flame cutting for steel structures should be seen not as such but for its use in conjunction with a cutting process. In the PTXSON configuration the flame itself is used for preheating and a separate oxygen stream is used for the cutting jet.
This capability is especially crucial for consumers looking to generate oxyhydrogen cutting solutions for carbon steel, since the generator doesn’t remove the necessity of cutting oxygen.
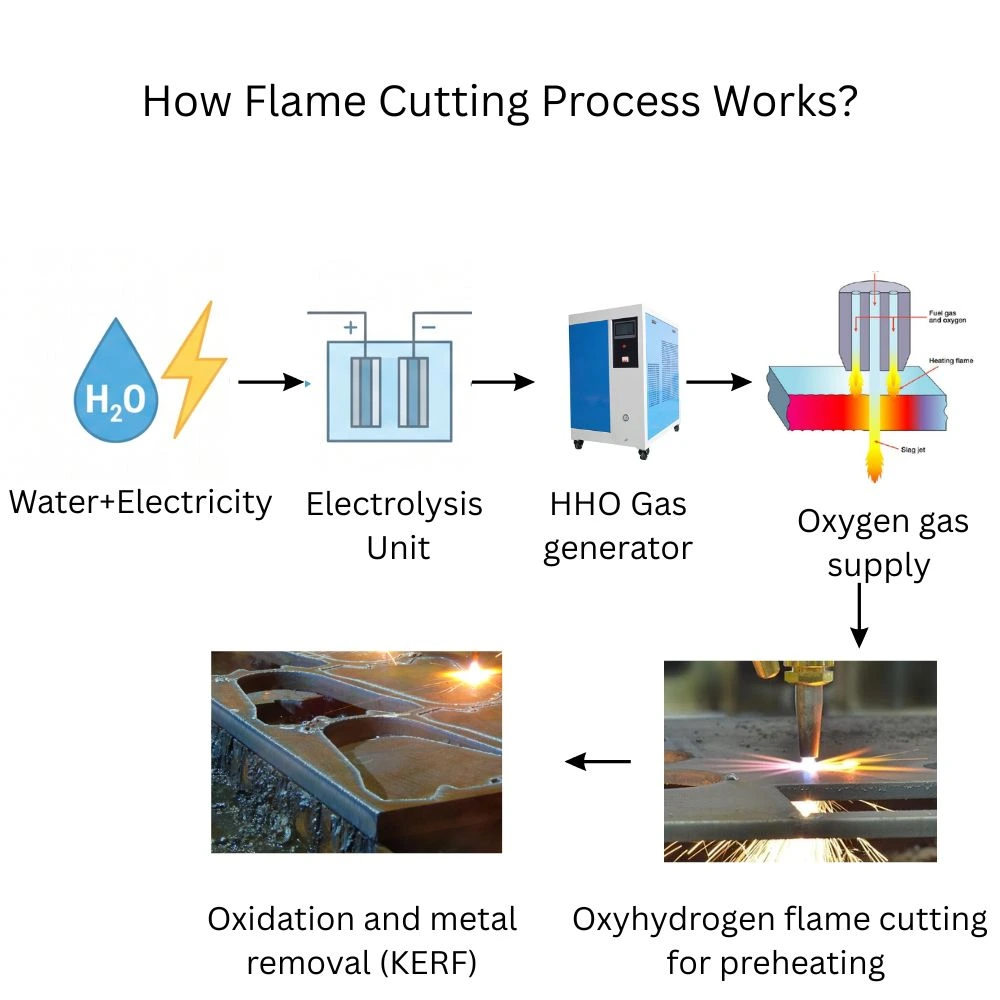
The oxyhydrogen cutting process starts by providing water to oxygen-hydrogen generator which receives electric energy, and it produces oxygen and hydrogen gas inside. This gas is used to drive the preheating torch, which melts the carbon steel to a certain ignition temperature. Then there is a cutting oxygen jet that is fed with heated steel, which allows oxidation and material removal, finalizing the cutting process.
The cutting oxygen supply is different: Oxygen cylinder/supply → Cutting oxygen line → Cutting torch → High pressure oxygen jet → Carbon steel. High-speed oxygen jet cuts material by reacting with the preheated steel and causing oxidation. This is important to distinguish because the preheating flame is provided by the oxyhydrogen generator and the cutting is done by the supply of oxygen. So, the oxyhydrogen generator can’t be used as an alternative to the cutting oxygen cylinder or supply.
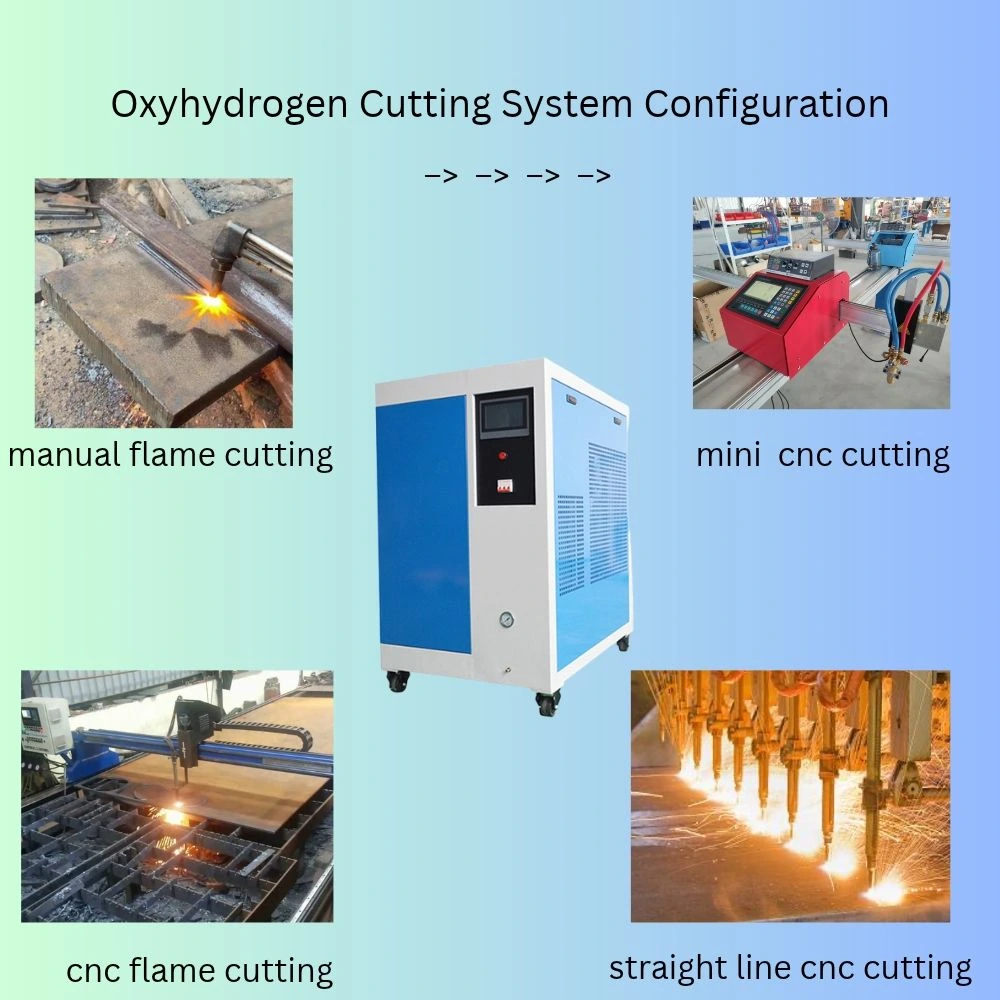
A PTXSON oxyhydrogen cutting for carbon steel system is a system that merges an oxyhydrogen generator and a carbon steel oxyhydrogen cutting torch with the ability to work with oxyhydrogen and a separate oxygen supply. There is a meaning given to each piece in cutting.
The cutting stove requires oxyhydrogen gas, which is obtained by the electrolysis of water. The system produces the necessary gas on site, as opposed to being dependent on a stored fuel gas for the preheating flame.
The actual oxyhydrogen gas generator’ capacity would depend on the amount of gas required, the operating hours, the torch type to be used in the operations, and the cutting load.
For industrial cutting use, the advantage of purchasing an industrial HHO generator for cutting should be reconsidered by taking into account the following: Gas output, operating parameters, electrical parameters, installation parameters and compatibility with cutting machinery.
These oxyhydrogen gas produced will be fed through appropriate equipment for working with the gas into a proper cutting torch. Preheating flame is produced by the torch itself and it is achieved by burning the gas.
This flame is to play a crucial role in preheating the carbon steel to the required temperature before the introduction of the cutting oxygen.
Therefore, the HHO flame cutting CO is important for carbon steel depends on the right combination of the generator output, gas flow, torch design and the properties of the carbon steel.
An oxygen cylinder, bulk oxygen system, and/or another oxygen source are used to supply the cutting oxygen separately.
It is an important component of the PTXSON configuration. It is not to be assumed that the generator is used for every share of the oxygen needed for the cutting operation, with the oxyhydrogen cutting system.
The gas from the oxyhydrogen generator is used for the preheating flame and the oxygen source is for the high pressure cutting jet.
When the carbon steel is at the desired preheating state, the cutting oxygen jet is turned on. The heated steels oxidize with the presence of oxygen and the products are blown off through the kerf.
A number of factors determine the resulting cut, such as:
Therefore it is recommended that an oxyhydrogen steel cutting system should be used for investigation on the application of use and not by any single performance figure.
When cutting carbon steel with oxyhydrogen, both types of cutting require the preheating flame to follow a separate cutting jet of oxygen. The only major difference with the PTXSON configuration is the configuration of the fuel.
In oxyhydrogen cutting compared to an oxy-fuel system, the oxyhydrogen system creates hydrogen oxygen gas on site for use in preheating the gases, instead of using bottled or distributed fuel gases like oxyhydrogen vs propane cutting as typical in the oxy-fuel systems.
This cutting mechanism is still the principle of carbon steel cutting by reaction of heated carbon steel and the cutting oxygen jet.
These are important differences between the two carbon steel flame cutting system.
| Comparison factor | PTXSON oxyhydrogen cutting configuration | Conventional oxy-fuel cutting |
| Preheating fuel | Hydrogen-oxygen gas generated onsite | Commonly acetylene, propane or another compatible fuel gas |
| Cutting oxygen | Separate oxygen cylinder or supply | Separate oxygen cylinder, bulk or distribution supply |
| Fuel supply | Generator, water and electricity | Cylinders, tanks or gas distribution |
| Flame function | Preheating | Preheating |
| Cutting mechanism | Oxidation of preheated carbon steel by oxygen | Oxidation of preheated carbon steel by oxygen |
| Equipment configuration | Oxyhydrogen generator, compatible torch and oxygen supply | Fuel-gas supply, compatible torch and oxygen supply |
| Operating costs | Electricity, water, oxygen, equipment and maintenance | Fuel, oxygen, equipment and maintenance |
| Integration | Requires generator and torch compatibility assessment | Depends on existing fuel and torch configuration |
| Main evaluation factors | Gas output, power use, flame performance, safety and cutting quality | Fuel consumption, flame characteristics, safety and cutting quality |
Typically the preheating fuel is used as fuel gas in a conventional oxy-fuel system. This can be in the form of acetylene, propane, or another suitable fuel – depending on the process.
In the PTXSON configuration, the onsite gas is manufactured by the industrial HHO generator that cuts into place.
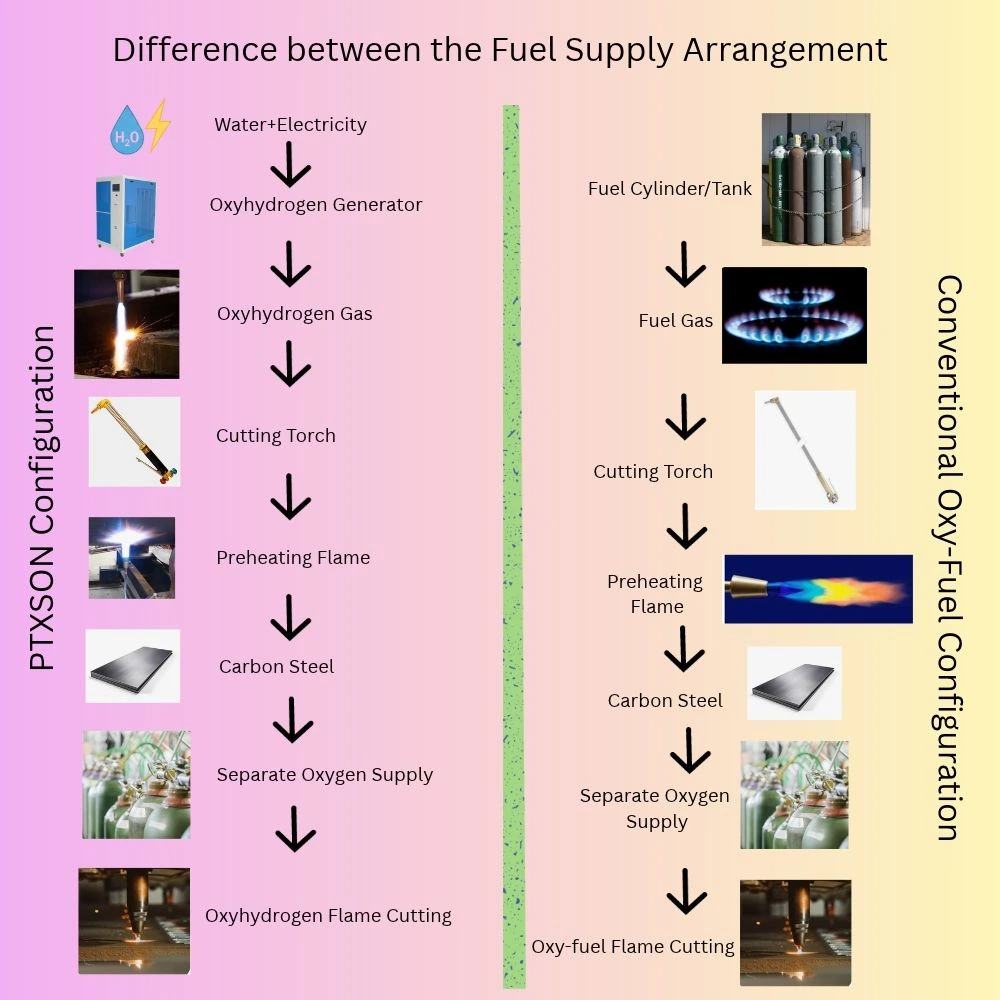
The water and electricity is used to fire the oxyhydrogen generator that supplies gas to a compatible cutting torch in the PTXSON configuration. This produces a flame which pre-heats carbon steel to the desired pre-heat temperature. At the same time, another oxygen supply produces a cutting oxygen jet which is reacted with the heated metal and thus creates an oxidation reaction to form the cut through the metal – the kerf. This set up enables a distinct separation of the preheating operation of oxyhydrogen from the cutting operation of the oxy-hydrogen jet cutting units.
A traditional gas-cutting system has fuel gas from a gas cylinder or gas tank delivered to a compatible gas cutting torch where the gas creates a preheating flame, which is used to bring the carbon steel to a desired temperature. A separate source of oxygen supplies a jet of oxygen gas at high pressure to the heated steel that reacts with the heated material to cause an oxidation reaction and remove material to create a kerf or cut in the material during the cut.
This comparison offers a practical comparison between oxyhydrogen vs oxy-fuel cutting; it should by no means be assumed to mean the higher performance method for any and all applications.
The decision of whether an oxyhydrogen cutting system is required, compared to other fuel arrangements is not solely based on the fuel itself. When evaluating for an industrial buyer, consider the entire cutting process.
When evaluating an oxyhydrogen system, consumers need to take into account the electric power needed by the generator, the amount of water needed, equipment costs, maintenance and the cost of a separate cutting oxygen supply.
In conventional systems, fuel-gas, oxygen and cylinder gas/Bulk gas consumption and supply logistics should be considered.
For a valid comparison between oxyhydrogen cutting vs conventional cutting, actual operating conditions from the process to be used should be applied.
Practical trials should be used to assess carbon steel oxyhydrogen cutting quality.
Some measurements that apply are:
The parameters used to cut carbon steel with oxyhydrogen boils down to whether the cut is required for the buyer’s production needs.
If an industrial user is interested in comparing them, make sure they operate under the same conditions.
The test shall take into account material grade, thickness, torch configuration, nozzle, oxygen pressure, conditions of preheating, the work operator and machine.
This is more informative than just comparing the nominal properties of the fuels.
Fuel-supply arrangement for the preheating flame has changed onsite generation, but a proper supply of oxygen is still needed for the cutting process.
So, customers need to evaluate generator installation, the supply of electricity, water, oxygen-cylinder logistics and gas handling, and available operating space.
Depending on the application, with both oxyhydrogen and conventional oxy-fuel cutting, there are different safety procedures that must be employed.
The following are industrial controls that should be set up by industrial users: Gas generation controls, Gas handling controls, Oxygen supply controls, Electrical equipment controls, Ventilation controls, Ignition source controls, Pressure controls, Torch operation and maintenance controls.
The training of operators is to be based on the specific set-up of the equipment and local safety requirements as applicable.
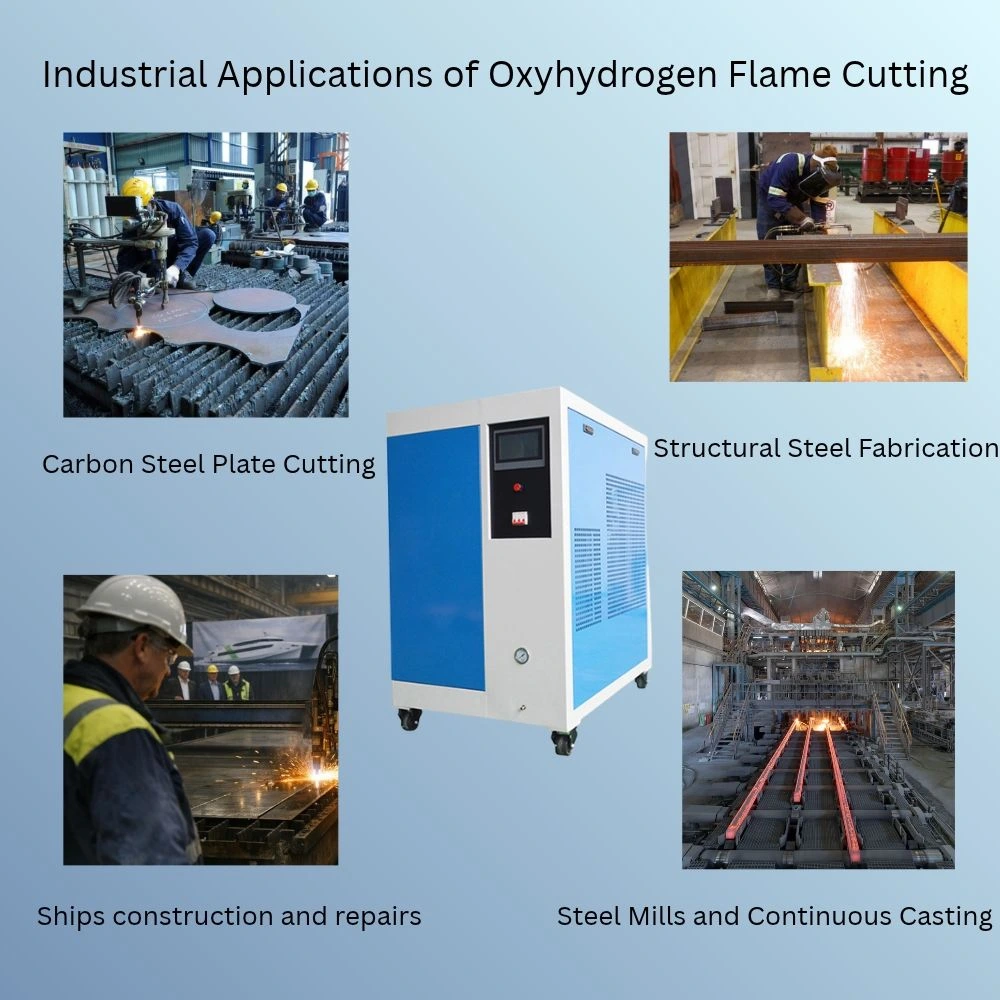
The carbon steel oxyhydrogen cutting may be considered in process workshops and production places where the carbon steel plate is subjected to an oxyhydrogen thermal cutting process.
Applications may include preparation of components, fabrication blanks, repair work and general steel processing.
Weighing the benefits of oxyhydrogen cutting for steel fabrication, steel fabricators utilizing beams, frames, supports and structural components might consider oxygen/acetylene cutting if a generator/torch combination is part of the process.
Oxyhydrogen flame cutting on a structural steel is a structural application that can be considered on the basis of material thickness, cutting geometry, quantity of production, torch movement, and the type of required edge condition.
Any oxyhydrogen steel fabrication equipment package can contain the oxyhydrogen generator, the gas-delivery comparatively, and a fitting and matching torch and oxygen supply, contingent on the application.
Some other applications are HHO cutting for steel fabrication,HHO flame cutting for carbon steel and oxyhydrogen cutting for metal fabrication.
Large carbon steel plates and structures are often shipped to shipyards for processing in the HHO flame cutting for shipbuilding and ship-repair industry.
An oxyhydrogen cutting for a ship-building application should be judged by plate thickness, cutting load, site conditions, supply of oxygen and the location and demand for generator(s) and torches.
For shipping repair work oxyhydrogen cutting for ship repair needs to be considered for portability, installation conditions, and access to the cut site.
One way to tackle the issues of a shipyard’s needs and the specifics of a particular job is to tailor the HHO cutting system for shipyards to the location and the specific job.
Examples of applications are HHO flame cutting for carbon steel in shipbuilding and oxyhydrogen steel plate cutting for shipyards.
Oxyhydrogen cutting for steel mills and continuous casting plants are required to cut billet, bloom and slab and to face tough requests for cutting.
Potential applications include:
These applications, however, will normally need a careful analysis of the engineering.
Buyers needing to incorporate an oxyhydrogen cutting system into a continuous production line should make sure to verify generator output, torch configuration, gas-flow, duty cycle, cutting speed, automation interfaces and process integration requirements.
One of the great advantages of an on-site oxyhydrogen system is that the gas produced in the preheating system can be produced at the point of use.
In appropriate applications, this affects the logistics of providing the preheating fuel. When the generator is powered by water and electricity, water and electricity are now considered inputs to the generator and the cutting jet’s oxygen supply is still required.
An industrial HHO cutting solution is based on this principle
It is possible to combine an oxyhydrogen steel cutting system with suitable hand or machine steel cutting equipment (technical assessment required).
The important thing is to match the gas flow and operating characteristics of the cutting torch to the gas flow and operating characteristics of the generator.
Prior to buying any industrial unit, the compatibility of the unit with the integration into the current oxy-hydrogen system must be evaluated.
In an oxyhydrogen vs acetylene cutting, the metal is heated with an oxyhydrogen flame before it is cut using a cutting oxygen jet. Be it in metal fabrication, steel processing, industrial manufacturing, or heavy equipment maintenance, it can be used in a wide variety of ways.
Key Benefits:
The type of system used is dependent on the thickness of material, type of torch configuration, cutting speed, and operating conditions.
Choosing an oxyhydrogen generator for cutting is the first to be in touch with the cutting process that is already in existence.
In an oxyhydrogen cutting system, the metal is first heated with an oxyhydrogen flame, and then cut by a cutting oxygen jet. It can be employed in a multitude of applications in metal fabrication, steel processing, industrial manufacturing, and especially with heavy equipment maintenance.
Prior to suggesting the use of a custom oxyhydrogen cutting system, PTXSON should be given information like:
The manufacturer of an oxyhydrogen generator can make a better determination of the application.
Technical support for a buyer who is weighing an oxyhydrogen generator supplier consist of the evaluation of the generator capacity, compatibility of the torch, installation conditions and the workload foreseen.
Contact PTXSON and they’ll take the time to see the material with you, discuss your torch configuration, and what fuel you use and the oxygen amount and fueling operating hours required for a technical visit.
For industrial applications, requiring a gas supply on site, PTXSON offers oxyhydrogen generation solutions which include thermal-processing and metal cutting processes compatible with the oxyhydrogen gas production. Choosing an appropriate system requires considerations to be given to generator capacity, gas output, torch compatibility, installation considerations and operating conditions.
Investigate the various PTXSON generator models, both in terms of the gas production capacity and the electrical requirements, as well as operating parameters and their suitability to a range of industrial applications.
Depending on project-specific needs, PTXSON can calculate an optimal configuration of generators, gas output and gas connecting method for the targeted cutting project.
Discover PTXSON manufacture procedures, specifications of manufacturing equipment and its quality control processes with verified information and genuine manufacturing documents.
Sends relevant technical documentation, installation instructions, operating instructions, maintenance instructions and after-sales services as required depending on services provided by the PTXSON.
Explore the potential of oxyhydrogen generators for combined and compatible industrial cutting, metal fabrication and thermal-processing processes. Application suitability should be determined based on the equipment specifications and on operational needs.
In search of an industrial oxyhydrogen generator? Talk to PTXSON about your application, production needs and equipment integration needs, and find an appropriate solution for your operation.
PTXSON can analyze the generator configuration for the actual cutting process when considering the carbon steel oxyhydrogen cutting.
For steel plates, structural fabrication, metal fabrication, oxyhydrogen cutting for shipbuilding, ship repair, or a potential oxyhydrogen cutting for continuous casting application, the right oxyhydrogen cutting system is based on the material thickness, torch configuration, gas-flow requirements, oxygen requirements and operating hours of your application.
These specifications can help PTXSON’s engineering team decide if an industrial HHO cutting equipment, custom oxyhydrogen cutting system or another configuration of the generator will best fit their application.
Oxyhydrogen HHO carbon steel cutting is a cutting process in which CO₂ gas is used as preheating gas and an oxyhydrogen gas flame is used for cutting. A well-designed oxyhydrogen cutting for steel plates system has the potential to shift the gas preheating supply paradigm by producing hydrogen and oxygen gas at the point of use in conjunction with electricity and water.
If the buyer is considering oxyhydrogen cutting, HHO cutting and/or an oxyhydrogen generator for cutting systems, the first step is to consider the entire cutting system against the actual cutting needs – generator output, torch type and combustion system, material thickness, productivity, cutting quality, safety, operating costs.